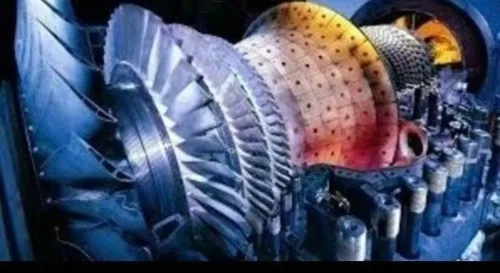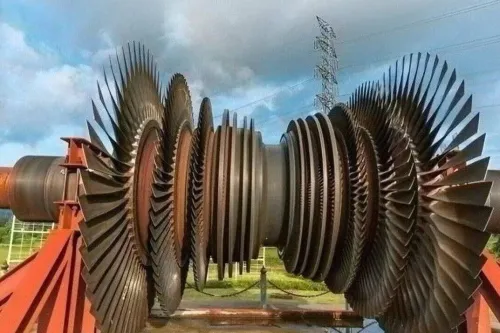

A damaged Nimonic 115 turbine blade cannot be approved for service because it looks clean after machining. You need a documented sequence that identifies cracks, creep, oxidation, dimensional loss and attachment damage, then proves whether recovery or replacement meets the engine’s approved limits.
Key takeaways
- Verify part number, stage, material, coating, identity, and damage history first.
- Reject recovery when cracks, distortion, or missing traceability exceed approved limits.
- Demand dimensional, coating, NDT, heat-treatment, and final inspection records.
- Compare HPT recovery quotations separately from intermediate-pressure blade replacement offers.
What high-pressure turbine blade recovery actually includes
A Nimonic 115 blade enters high-pressure turbine blade recovery as an identification and inspection problem, not a re-machining job. Verify its part number, engine stage, material, coating, serial or batch identity, and available damage history before selecting any repair.
1. Record the blade condition with visual examination and photographs, including missing material, erosion, burns, platform damage, shrouds, tip features, cooling-hole position and diameter, internal passages, and the fir-tree or dovetail attachment.
2. Perform fluorescent penetrant inspection to find open surface cracks. Use radiography or computed tomography for internal defects, weld regions, and blocked passages; use ultrasonic testing when the approved method supports subsurface or wall-condition checks.
3. Measure the airfoil against the approved datum system using a CMM, laser scanner, or structured-light scanner. Check profile, twist, lean, tip, platform, root datums, shrouds, cooling holes, and attachment geometry rather than comparing the blade by eye.
4. Section a sample for metallographic examination when microstructure, overheating, or crack morphology cannot be resolved nondestructively. Do not machine first: a crack left in the parent material can emerge at a blend edge after material removal.
Recovery ends with an initial engineering disposition against approved repair data, including crack, wall, coating, and dimensional limits. It is not generic cleaning or profile restoration; the blade is repairable, rejectable, or replaceable only within that documented scheme.
When recovery is acceptable—and when replacement is the safer decision
A damaged Nimonic 115 blade is recoverable only when its damage map fits the engine manual, OEM repair scheme or approved engineering limits. Compare crack length and location, minimum wall thickness, blend depth, tip reduction, platform distortion, airfoil twist, leading- and trailing-edge loss, oxidation depth and attachment condition before removing material.
No universal crack, wall-loss or tip-reduction limit applies; the part number and repair data control.
Use high pressure turbine blade recovery only within that envelope:
- Remove oxides and damaged material, then blend or restore the area without exceeding the permitted depth.
- Reject or replace the blade when a crack reaches a critical section, material loss breaches minimum wall, creep permanently distorts the airfoil or platform, foreign-object damage enters a cooling feature, or the root fails its datum requirements.
- Check whether the repair changes cooling flow, hole discharge, airfoil load distribution, platform sealing or attachment fit.
| Damage | Recovery decision | Main concern |
|---|---|---|
| Leading-edge dent | Blend if limits remain | Crack initiation and profile loss |
| Tip loss | Tip restoration if permitted | Clearance and mass distribution |
| Cooling-feature damage | Replace when passage or hole is altered beyond limits | Cooling flow and overheating |
A blade that looks correct can still fail functionally. Record each rejected blade by part number, serial or batch identity, damage map and exact disposition reason; do not return it to stock as an unidentified part.
Which repair and acceptance processes make a recovered blade serviceable
After disposition, remove oxide and cracked or overheated material, then blend within the approved depth and profile limits. Use alloy-specific weld build-up, qualified laser cladding, or brazing only where the approved repair calls for it. Restore the tip, finish-machine the airfoil and attachment, apply specified heat treatment, and record every parameter.
| Repair method | Required control | What failure can cause |
|---|---|---|
| Weld build-up | Filler-metal rationale, preheat, interpass temperature, repair parameters, crack-removal evidence and procedure qualification | Heat-affected-zone cracking or distortion |
| Laser cladding | Qualified process window, substrate temperature and deposited-layer inspection | Poor bonding or excessive heat input |
| Brazing | Approved braze alloy, joint clearance, furnace cycle and post-braze NDT | Voids, leakage or weakened repair |
| Tip restoration | Approved material, geometry, balance and finish-machining limits | Incorrect clearance or altered mass properties |
Nimonic 115 is a precipitation-strengthened nickel-base alloy, not stainless steel or low-alloy steel. Its gamma-prime-strengthened structure makes generic welding practice unsafe; ask for alloy-specific qualification results before accepting a repair.
Treat the substrate and thermal-barrier coating as separate operations. Remove the coating without damaging the substrate, verify bond-coat condition, prepare the surface, control coating thickness, mask cooling holes and inspect the finished coating.
- Complete final fluorescent penetrant inspection or the specified NDT.
- Compare CMM or scan results with the approved datum system; check cooling-hole position and diameter, root, platform, tip and airfoil geometry.
- Verify balance or mass properties when specified.
- Include heat-treatment and coating records, traceability and a signed conformity release.
NADCAP, ISO 9001 and AS9100 support process control; none approves a particular repair.
Why intermediate-pressure replacement is not an HPT blade swap
An intermediate pressure turbine blade replacement is not an HPT blade swap. The stages see different operating temperatures, gas loading and centrifugal loading, so their airfoil geometry, root attachment, shroud or platform design, cooling arrangement, coating system, balance requirement and allowable operating limits differ.
| Stage | Design factors | Replacement implication |
|---|---|---|
| HPT | Highest gas temperature; intense cooling demand; high thermal and centrifugal stress; complex airfoil, root, platform and coating features | Recover or replace only against HPT-specific approved data |
| IPT | Lower temperature than HPT, but distinct gas loading, rotor speed, geometry, attachment and mass-balance requirements | Use an IPT-specific blade, not a generic turbine-section part |
“Nimonic” does not identify an interchangeable blade. Match the intermediate pressure turbine blade replacement to engine model, stage, exact part number, revision, modification status and approved configuration.
A Nimonic 115 blade, another nickel-based superalloy or an Inconel grade may differ in temperature capability, density, repairability and oxidation resistance; titanium is lighter but may lack the required temperature strength, cooling compatibility or attachment capability.
| Material | Key trade-off |
|---|---|
| Nimonic 115 | High-temperature strength and oxidation resistance; repair and heat treatment require qualified controls |
| Other nickel alloys or Inconel | Chemistry, density, coating response and design compatibility vary by grade |
| Titanium | Lower density, but limited by temperature capability and original cooling or root design |
Require the material certificate, heat-treatment and coating records, dimensional report, NDT results, serial or batch traceability where required, and conformity documentation. Choose a new blade when the root, cooling passages or geometry exceed approved recovery limits; restoring the airfoil cannot correct an unsafe attachment or altered cooling flow.
How to qualify a Bengaluru supplier and request a comparable quotation
Compare suppliers across three separate capabilities; a strong 5-axis machine shop may subcontract the welding or coating that controls recovery success. Use the search phrase aero engine parts manufacturers nimonic turbine blade for recovery in bengaluru to find candidates, then ask whether each capability is in-house, subcontracted or part of a shop-based recovery program.
Use BVPL Turbine Parts as a Bengaluru option for comparing precision machining, inspection and turbine-component supply against your defined repair or replacement scope.
Send every bidder the same handoff package:
- Engine and stage; blade part number and revision; material and coating designation; serial or batch identity.
- Damage photographs and maps; operating history if available; required NDT; repair limits; quantity and acceptance standard.
- Required deliverable: repair, exchange unit or new replacement.
| Capability | Evidence to request | Sourcing question |
|---|---|---|
| Repair engineering and disposition | Approved repair data, damage limits and signed disposition | Who decides repair versus rejection? |
| Welding, heat treatment and coating | Alloy-specific procedure qualifications, parameters and outsourced-process controls | Who performs each special process? |
| CNC machining and inspection | Calibrated-equipment records, sample dimensional reports and final NDT method | Which datums and acceptance standard govern release? |
Do not treat “TIG welding available” as qualification. Also request traceability, material and heat-treatment records, coating records, and conformity documentation. If screening a nimonic 115 turbine blade manufacturer in bengaluru, verify process-specific evidence rather than relying on NADCAP, ISO 9001 or AS9100 alone.
Related service
Aero Engine Blade High Pressure Turbine and Intermediate Pressure Turbine Blades Material: Nimonic 115 High Pressure & Intermediate Pressure Turbine Blades Material: Nimonic 115 Nimonic 115 is a high-performance nickel-chromium-cobalt alloy engineered... |
Frequently asked questions
What does high-pressure turbine blade recovery include?
It includes identity verification, dimensional inspection, coating assessment, damage mapping, approved repair, NDT, restoration, and final acceptance checks.
When is recovery acceptable instead of replacement?
Recovery is acceptable when damage remains within approved repair limits and inspection proves restored dimensions, material condition, coating, and traceability.
Why is intermediate-pressure blade replacement different from HPT blade recovery?
Intermediate-pressure replacement involves supplying and qualifying a replacement part, while HPT recovery evaluates and restores an existing blade with stricter damage and life limits.
How should you qualify a Bengaluru turbine-parts supplier?
Request evidence of relevant manufacturing and repair capability, traceability controls, inspection methods, acceptance records, lead time, exclusions, and a line-item quotation.