
A damaged Nimonic 115 blade is not automatically an immediate-shutdown finding, but neither is it a cosmetic issue. Operators need to connect the defect’s location and morphology with vibration, exhaust-gas-temperature spread, efficiency, operating history and approved repair limits before choosing continued operation, inspection escalation, repair or replacement.
Key takeaways
- Shut down when damage risks material release, imbalance, or downstream hardware impact.
- Use vibration, exhaust temperature, borescope, and trend data to confirm blade failure.
- Crack direction, oxidation, erosion, and foreign-object marks reveal likely failure mechanisms.
- Repair only within approved limits; replace blades with critical cracks, distortion, or section loss.
When Does Nimonic 115 Blade Damage Require Shutdown?
Shutdown is required when Nimonic 115 blade damage threatens material liberation, rotor balance, or downstream hardware. The practical Nimonic 115 blade damage meaning is determined by defect severity, location, trend data, and the engine maker’s approved limits—not by appearance alone.
- Immediate shutdown: Stop the engine for liberated material, a growing crack, severe tip loss, shroud contact, a rapid vibration change, a large EGT spread, or evidence of downstream damage. A rotating blade can release fragments into later stages, damage seals, and create imbalance within seconds.
- Restricted operation: Continue only within the engine maker’s written limits when the defect is stable, measured, and below rejection criteria. Record vibration, EGT spread, operating hours, and cycles before every required inspection.
- Inspection escalation: Send the finding for borescope mapping, dimensional checks, and approved crack detection when a minor documented dent, isolated coating loss, unusual tip clearance, or new trend lacks a clear disposition.
- Planned replacement: Schedule removal when the blade remains serviceable today but approaches life, repair, coating, tip, or profile limits.
Do not apply rotating-blade logic to a stationary vane. A blade defect can cause imbalance and liberation; vane damage more often changes flow area, blocks cooling passages, cracks a platform, or reduces nozzle efficiency. Clear cockpit trends do not excuse a suspected crack.
Which Symptoms Point to Nimonic 115 Blade Failure?
Monitor these Nimonic 115 blade failure symptoms before and after a suspected event:
- Rising turbine vibration at rotational frequency or blade-passing frequency
- A widening exhaust-gas-temperature spread between engine cans or probes
- Reduced compressor or turbine efficiency, shown by performance-trend deterioration
- Rising fuel flow for the same thrust or power output
- Reduced EGT margin
- Abnormal whine, rubbing, imbalance or other engine noise
- A change in measured tip clearance
- Metal debris in filters, oil systems where applicable, or borescope findings such as missing, distorted or cracked airfoil material
A clean cockpit trend does not clear a blade. A small crack can remain symptom-free until propagation, so a normal vibration trace cannot replace a borescope inspection or approved engineering assessment.
The damage pattern also depends on the pressure section:
| Pressure section | Typical damage | Useful warning signs |
|---|---|---|
| High-pressure turbine | Creep, oxidation, hot corrosion, cooling-hole cracking, trailing-edge distress and tip damage from extreme temperature | EGT spread, reduced margin, changed clearance, efficiency loss and borescope distortion |
| Intermediate-pressure turbine | FOD, erosion, platform or root cracking, corrosion and vibration-driven fatigue | Vibration at resonant or blade-passing frequencies, noise, debris, profile loss and cracking near attachments |
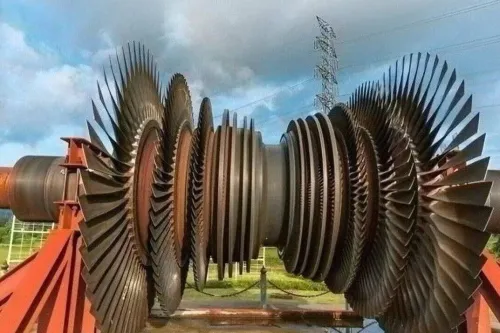
High pressure turbine blade damage carries a smaller thermal and remaining-life margin because the stage sits directly behind the combustor. Intermediate pressure turbine problems can still become severe: longer exposure, resonant behavior and high-cycle fatigue can drive failure even at lower gas temperature.
Trend data narrows the search; it does not establish crack size or safe operating life.
What Does the Defect Shape Reveal About the Failure Mechanism?
Airfoil shape is a clue, not a diagnosis. Interpret it with stage, location, operating hours, cycle history and inspection evidence; a burned-looking area can reflect overheating, oxidation, hot corrosion, a coating failure or a prior repair.
1. Elongation, bowing, permanent twist or altered tip clearance point toward creep: time, temperature and stress have changed the airfoil’s geometry. Distorted platforms, shrouds, cooling holes or trailing edges strengthen that concern, even when the surface remains intact.
2. Scale, recession and coating loss indicate oxidation or hot corrosion exposure. Liberated coating exposes the Nimonic 115 substrate to faster attack; burned or missing material means section loss, not merely discoloration. Measure profile loss and remaining wall thickness before accepting continued operation.
3. Cracks at cooling holes, platform fillets, shrouds, trailing edges or repair blends fit thermal-mechanical fatigue because those features concentrate stress during temperature cycles. A crack hidden at a blend boundary can remain dangerous after material is removed.
4. Leading-edge dents or gouges are consistent with foreign-object damage. Tip rubs and shroud contact show interference or clearance change; platform cracking threatens load transfer, trailing-edge erosion changes flow, and blocked cooling passages raise local metal temperature.
For disposition, record crack length and location, remaining wall thickness, profile loss, liberated material and passage blockage. A rotating blade also demands attention to imbalance and possible liberation, while a vane more often suffers flow-area or nozzle-efficiency loss. Confirm the mechanism with dimensional checks, crack testing and metallurgical evidence; discoloration alone cannot establish risk.
How Should Operators Confirm the Damaged Stage and Part Condition?
Do not approve continued operation from a single dark mark or borescope photograph. Build an evidence trail that identifies the damaged stage, establishes the defect’s extent and links it to the correct engineering limits.
1. Record the exact engine model, pressure section, stage, blade part number, serial or batch traceability, operating hours, cycles, prior repairs and coating history. Include clear borescope images from multiple angles, with scale references showing the leading edge, trailing edge, tip, platform, shroud and cooling holes.
2. Map every crack indication by location, length and orientation. Measure airfoil chord, thickness, twist, bow, elongation, tip clearance, blend depth and cooling-hole geometry against the engine maker’s limits. A profile loss or dimensional change can matter even when no crack is visible.
3. Use fluorescent-penetrant inspection, or dye penetrant where approved, to find surface-connected cracks. Penetrant will not reliably reveal a closed internal flaw, so do not treat a clean result as a complete clearance.
4. Select eddy-current, radiographic or metallographic examination when the geometry, suspected flaw and engineering data justify it. Use metallography to investigate creep, oxidation, coating penetration or unsuitable repair when removing a sample is authorised; radiography is not a universal substitute for surface-crack inspection.
5. Correlate the findings with vibration at rotational and blade-passing frequencies, EGT spread and margin, engine trend data, debris findings and maintenance records. This evidence helps separate HPT damage from IP damage and supports operation, repair or replacement decisions.
Nimonic 115 designation alone proves neither interchangeability nor dimensional fit. Release the part only against the approved configuration, inspection limits and disposition authority.
Should You Repair or Replace a Nimonic 115 Blade?
1. Repair the blade only when the engine maker’s repair manual or an approved type-design scheme explicitly covers the finding. The approval must match crack location and size, blend depth, minimum wall thickness, tip condition, platform distress, cooling-hole geometry, coating condition and remaining life.
A generic “maximum blend depth” is not enough; blending can leave a crack at the blend boundary.
2. Replace the blade when material has been liberated, the airfoil profile is outside limits, creep has consumed its approved life, cooling passages remain blocked beyond the authorised restoration, or serial traceability is incomplete. A rotating blade carries imbalance and liberation risk, so a clean cockpit trend does not justify continued use.
3. Do not substitute another hot-section blade because its alloy appears comparable. A different alloy, coating system, cooling design, geometry or approved repair process can change strength, airflow, clearances and life limits. Confirm the exact part number, stage and type-design approval before accepting an alternative.
4. Demand a release package from any supplier. It should include process qualification, NDT records, material-certification and heat-treatment evidence, repair authority, coating inspection, dimensional results, serial traceability, repair history and cycle or exposure accounting.
When evaluating a turbine blade manufacturer in Bengaluru, including BVPL Turbine Parts, ask who holds disposition authority and which approved data supports the work. AS9100 supports quality-system confidence; it does not approve a life-limited part.
Related service
Aero Engine Blade High Pressure Turbine and Intermediate Pressure Turbine Blades Material: Nimonic 115 High Pressure & Intermediate Pressure Turbine Blades Material: Nimonic 115 Nimonic 115 is a high-performance nickel-chromium-cobalt alloy engineered... |
Frequently asked questions
When does Nimonic 115 blade damage require shutdown?
Shut down when damage threatens material liberation, rotor balance, or downstream hardware. Use the engine maker’s approved limits, defect location, and trend data rather than appearance alone.
Which symptoms point to Nimonic 115 blade failure?
Rising vibration, exhaust-gas-temperature spread, compressor or turbine efficiency loss, abnormal metal temperature, and foreign-object damage can indicate failure. Confirm these signs with borescope inspection and operating trends.
What does the defect shape reveal about the failure mechanism?
A sharp crack can indicate fatigue, evenly distributed thinning points to erosion, oxidation and creep suggest high-temperature exposure, and local dents or tears indicate foreign-object damage.
How should operators confirm the damaged stage and part condition?
Correlate borescope images with engine records, vibration data, exhaust-temperature patterns, and stage-specific inspection references. Record the blade position, defect dimensions, crack direction, and surrounding hardware condition.
Should you repair or replace a Nimonic 115 blade?
Repair when the defect fits the approved repair scheme and remaining dimensions meet limits. Replace the blade when cracking, distortion, section loss, or liberated material exceeds those limits.